- Home
-
Products Center
Products Center
-
Solutions
Solutions
- Service Support
- News Center
- Blog
- About Us
- Contact Us


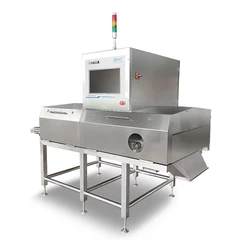
Commercial Colour Sorter Machine & Optical Sorting Solutions
Designed for demanding agricultural and industrial sorting needs across European, Asian, and African markets. Enhance product purity up to 99.99% with multi-spectral CCD and NIR optical colour sorting technology.
- High-Resolution Industrial Optics — 5400-pixel RGB/CCD sensors detect minute colour variations, spots, and surface defects
- AI-Powered Deep Learning — Self-learning algorithms simplify calibration for changing raw material batches
- Durable Ejector System — High-frequency smart valves, ultra-low air use, 10+ billion cycle lifespan
- Global Voltage & Compliance — 220V/380V/415V, 50/60Hz, with CE and ISO for worldwide installation
Primary Applications for Colour Sorting Machines
Engineered for a wide range of agricultural and industrial materials — also referred to as a color sorter in some markets.
Grain & Paddy Processing
High-throughput separation of chalky grains, discoloured rice, and foreign objects. Ideal for automated rice milling line integration.
Seeds, Pulses & Nuts Sorting
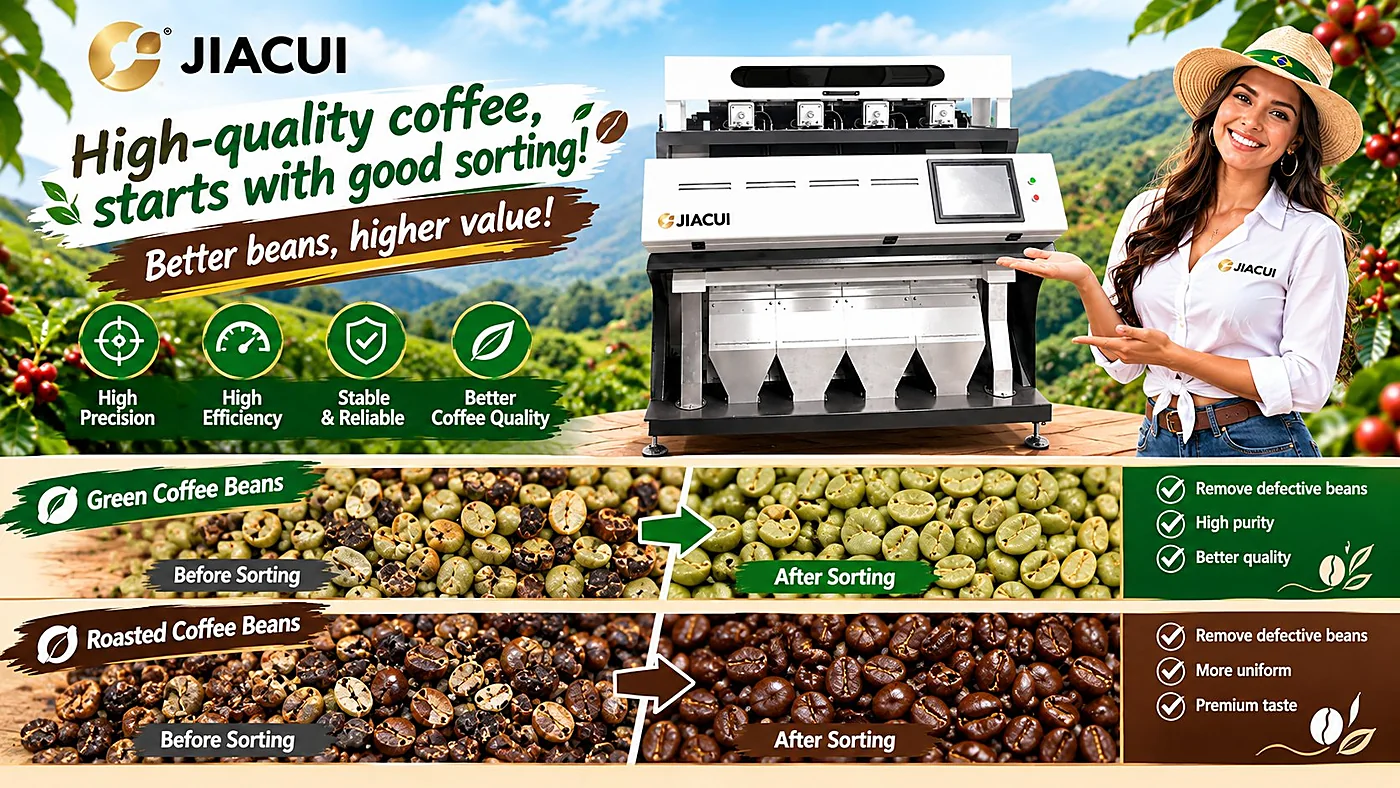
Precision optical colour sorter machines tailored for lentils, sesame, coffee beans, cashews, and peanuts. Minimise yield loss while maintaining grade consistency.
Recycling & Polymers Separation
Advanced belt and chute type colour sorting equipment for separating mixed PET flakes, HDPE granules, and metallic residues.
Technical Features & Engineering Highlights
High-Resolution Industrial Optics
Equipped with 5400-pixel RGB/CCD sensors that detect minute colour variations, spots, and surface defects.
AI-Powered Deep Learning Algorithms
Self-learning algorithms simplify calibration for workers, ensuring steady sorting efficiency across changing raw material batches.
Durable Ejector System
High-frequency smart ejector valves with ultra-low air consumption and an extended service lifespan (over 10 billion cycles).
Global Voltage & Compliance
Configured to international electrical standards (220V/380V/415V, 50Hz/60Hz) with CE and ISO certifications for worldwide installation — ideal for UK, India, and Southeast Asia.
Frequently Asked Questions About Colour Sorter Machines
Answers from our sorting engineers. Something else on your mind? Ask us directly →
How does a modern colour sorter machine work?
Can your colour sorting machines be customised for local crop types?
What capacity ranges do your colour sorter machines support?
Upgrade Your Processing Line with a High-Value Colour Sorter Machine
Send us your raw material samples for a free sorting test video and a personalised purity analysis report.