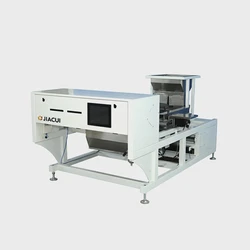



The complaint that reaches us most often from rice mills is not "the machine stopped". It is "the machine is throwing away too much good rice". A sorter that runs perfectly but over-ejects is quietly destroying margin every shift, and because nothing is broken, nobody investigates.
This article covers the seven faults that cause high carry-over and missed defects on rice lines, in the order we find them in the field, followed by a printable maintenance schedule you can hand to the shift supervisor.
First, separate the two symptoms
Before touching any setting, establish which problem you actually have. They have different causes and different fixes, and operators routinely treat one as the other.
| Symptom | What it means | Typical root cause |
|---|---|---|
| Defects pass through (missed) | Detection is not seeing them | Dirty optics, uneven feed, sensitivity too low, wrong recipe |
| Good rice is ejected (carry-over) | Detection or ejection is firing too broadly | Sensitivity too high, valve timing, air pressure, overlapping feed |
| Both at once | Usually a presentation or air problem | Feed surges, wet air, worn valves |
If both symptoms appear on the same shift, resist the urge to change sensitivity first. Sensitivity is a software knob; most Pakistani, Indian and Southeast Asian mill faults we see are mechanical or pneumatic.
1. Air supply problems — the most common cause
Ejector valves run on compressed air, and rice dust makes the air system a wear item. Three failure modes dominate:
- Pressure instability. When line pressure sags during a shift, ejection force drops and the valve dwell time lengthens to compensate — which blasts neighbouring kernels. The result is missed defects and extra carry-over, simultaneously.
- Water and oil in the line. Poor filtration lets condensate and oil reach the valves, causing sticking and delayed response. A valve that fires 2 ms late ejects the kernel behind the target.
- Leaking or worn valves. A valve that never fully closes keeps a nozzle open, producing a continuous narrow blast of good rice into the reject stream. This is one of the most invisible forms of loss in a mill.
Check the air system before adjusting any recipe. Confirm regulated pressure at the machine, drain the receiver and filters on schedule, and inspect for valves that stay open when the machine is idling. The working principle is covered in our guide to the ejection system.
2. Dirty optical windows and mirrors
Rice bran is oily and abrasive. It does not simply dim the camera — it scatters light and creates a haze that the machine reads as low contrast. Two consequences follow: genuine defects fall below the detection threshold, and operators raise sensitivity to compensate, which then over-ejects.
This is why "clean the glass" is not housekeeping; it is calibration. Practical rules:
- Operator cleaning at every shift change on rice lines. Bran accumulates fast enough to measurably affect detection within a single long shift.
- Check the air curtain. If the protective air flow is weak or misdirected, dust reaches the windows continuously and no cleaning frequency will keep up.
- Inspect lamps and light sources on the same schedule. Aged lamps shift colour temperature, which silently changes what the machine considers "yellow".
3. Uneven feed and kernel overlap
A color sorter can only judge what it can see individually. When the feed surges, kernels overlap and the camera reads an average of two or three surfaces. Chalky kernels disappear into the average; yellow grains look paler than they are.
Common causes of uneven presentation:
- Vibratory feeder running too full. The single most frequent error. Feed rate should be set so the chute carries a single, continuous layer — not the maximum the machine will accept.
- Chute wear or contamination. Rough or dirty chute surfaces cause grains to bounce, creating gaps and clusters downstream.
- Hopper bridging. Rice can bridge above the feeder, producing a starved then overloaded pattern that looks like a machine fault.
- Level control instability. If the buffer level oscillates, so does feed density.
Before changing any sensitivity value, watch the chute for a full minute. If the layer is not even, no parameter change will fix the result. The physics is explained in material presentation and feeding.
4. Sensitivity raised to mask another problem
Sensitivity is the setting operators reach for first and should reach for last. On rice, raising sensitivity to catch a few remaining defects typically costs far more good grain than it recovers in defects — the classic trade that produces high carry-over.
A disciplined approach:
- Fix optics, air and feed first. Then evaluate whether sensitivity genuinely needs to change.
- Change one parameter at a time and re-weigh both streams. If you cannot measure the change, you cannot manage it.
- Store recipes per product. White, parboiled, basmati and coloured rice should not share a setting.
The measurement discipline itself is covered in fixing over-rejection.
5. Wrong or copied recipe
Recipes migrate between machines and between products. A recipe copied from white rice applied to parboiled rice will classify normal amber kernels as defects and produce enormous carry-over. A recipe copied from a different origin may be slightly off in colour space and cause chronic low-level loss that nobody notices.
Build recipes from your own material: run the batch, inspect the accept stream and the reject stream, and adjust the reference until the reject stream is concentrated rather than diluted.
6. Mechanical wear at transfer points
Worn chutes, misaligned feeders and damaged elevator buckets do not cause sorting errors directly — they cause breakage. And breakage creates brokens, which then either fail the grade or get ejected as defects, adding to apparent carry-over.
On basmati and other long-grain rice, this is a significant hidden loss. Inspect transfer points monthly, and treat a rise in broken content as a mechanical signal before assuming it is a sorting problem.
7. Environmental and electrical drift
Rice mills are hot, humid and dusty. Ambient temperature changes affect camera sensors and light output; unstable power affects both. Symptoms appear as a machine that "works in the morning and drifts by afternoon".
Mitigations that cost little:
- Keep the control cabinet sealed and filtered, and check that cabinet cooling is working.
- Use voltage stabilization if the site supply fluctuates.
- Recalibrate after any lamp replacement, and log it.
- Run a reference sample through the machine periodically and compare against the previous result — a simple drift test that catches most of these issues before the buyer does.
Daily, weekly and monthly checklist
Print this and attach it to the machine. The value is in the routine, not the document.
| Frequency | Task | Why it matters |
|---|---|---|
| Every shift | Clean optical windows and mirrors | Bran haze is the leading cause of missed defects |
| Drain air filter / receiver | Condensate causes valve sticking | |
| Watch chute for even single-layer feed | Overlap destroys low-contrast detection | |
| Weigh accept vs reject samples | Only measurement reveals carry-over drift | |
| Weekly | Check regulated air pressure at the machine | Pressure sag causes both missed and over-ejection |
| Inspect valves for stuck-open nozzles | Silent continuous loss into reject | |
| Verify air curtain flow | Weak curtain means constant dust on optics | |
| Monthly | Inspect chutes and transfer points for wear | Wear creates brokens that look like sorting faults |
| Check lamp hours and colour stability | Aged lamps shift the yellow threshold | |
| Run a reference sample drift test | Catches calibration drift early | |
| Review recipes against current lots | Origin changes require recipe updates |
A longer version with seasonal items is in our general color sorter maintenance checklist.
When the machine is the problem, not the settings
If optics are clean, feed is even, air is stable and the recipe is correct, yet carry-over remains high, the limit is usually hardware: sensor resolution, illumination design, or valve response. On older machines this is a genuine ceiling, and no amount of tuning will move it.
At that point the question becomes economic rather than technical. Compare the annual value of the rice you are losing against the cost of a machine designed for low-contrast rice sorting. On a mill running multiple shifts, that comparison usually resolves quickly — an improvement of even half a percentage point in carry-over is significant money.
FAQ
Why is my rice sorter blowing good rice into the reject stream?
Check, in order: air pressure stability, valves stuck open, sensitivity set too high, and feed overlap. Roughly three-quarters of the cases we see are pneumatic or presentation-related rather than software.
How often should optical windows be cleaned?
Every shift change on rice. Rice bran is oily and accumulates fast; a full shift without cleaning measurably degrades chalky-kernel detection.
Does higher sensitivity remove more defects?
It removes more of everything, including good rice. On low-margin rice, the carry-over cost usually exceeds the value of the extra defects caught. Fix the physical causes first.
What carry-over ratio should I expect?
It depends on the machine, the defect load and the recipe. Ask for the figure at your target purity, not the headline accuracy. If a supplier cannot state carry-over at a defined condition, the accuracy claim is not comparable.
Next step
Work through the list in order — air, optics, feed, then settings. Most mills recover a measurable share of lost rice without buying anything.
See the capability bands in the rice and grain color sorter range if your current machine is at its hardware limit, and read the over-rejection guide for the measurement method. If you would like us to review your settings and reject stream, send us a sample and your current parameters.